
Mastering 316L Stainless Steel Fabrication: Essential Techniques and Best Practices for 2026
The intricacies of working with specialized materials often present a steep learning curve. When it comes to 316L stainless steel fabrication, the challenges extend beyond general metalworking, demanding a deep understanding of its unique metallurgical properties and precise handling protocols. Without this specialized knowledge, fabricators risk compromising the material's inherent advantages, leading to costly reworks or, worse, premature equipment failure in critical applications. This article unpacks the essential techniques and best practices to successfully fabricate 316L stainless steel, ensuring optimal performance and longevity for manufactured components.
The Unique Material: Understanding 316L Stainless Steel
316L stainless steel is a low-carbon variant of the standard 316 grade, known for its superior corrosion resistance compared to many other alloys. This characteristic makes it a preferred choice for environments where exposure to aggressive media is common. Its composition includes molybdenum, which enhances its resistance to pitting and crevice corrosion, particularly in chloride-rich settings. For industries demanding stringent hygiene and durability, such as pharmaceutical, medical, and food processing, 316L is frequently specified for equipment components that come into direct contact with products. Its ability to resist attack from various substances ensures material integrity and prevents contamination, upholding critical cleanliness standards.
The "L" in 316L signifies its lower carbon content, typically 0.03% maximum, compared to the 0.08% maximum in standard 316. While this low carbon content is often highlighted for its role in mitigating carbide precipitation during welding (a phenomenon that can lead to intergranular corrosion), its practical implication in fabrication is nuanced. Fabricators must maintain careful control over heat input during processes like welding to preserve the material's advantageous properties, ensuring the finished product performs as expected. For a broader context on stainless steel types, exploring articles on Stainless Steel can provide foundational knowledge.
Foundational Steps in 316L Stainless Steel Fabrication
Successful 316L stainless steel fabrication begins with meticulous planning and execution of fundamental processes. Unlike working with materials such as mild steel, 316L requires specific considerations at every stage to prevent contamination and maintain its critical properties.
Material Handling and Preparation
Proper material handling is paramount to avoid surface defects and cross-contamination. 316L sheets and components should be stored separately from carbon steels and other alloys to prevent iron particle embedment, which can compromise its corrosion resistance. Tools used for 316L should be dedicated or thoroughly cleaned to ensure they do not introduce foreign contaminants. Preparation often involves precise cutting to achieve the desired dimensions. Common methods for cutting 316L include shearing, laser cutting, and waterjet cutting. These techniques are chosen based on the thickness of the material, precision requirements, and the need to minimize heat-affected zones.
Shaping and Forming Operations
Once cut, 316L stainless steel can be shaped through various forming operations. These include bending, rolling, and stamping. While 316L generally exhibits good formability, its higher strength compared to some other stainless steels means that more force may be required for forming. Fabricators must account for its spring-back characteristics, which are often more pronounced than in lower-alloy steels, to achieve accurate angles and curvatures. Careful tooling selection and machine calibration are essential to prevent surface marring and maintain dimensional accuracy.
Machining 316L Stainless Steel
Machining 316L stainless steel, like other austenitic grades, presents specific challenges due to its work-hardening tendencies and high ductility. This means the material can become harder as it is cut, leading to increased tool wear and difficulty in chip removal. Best practices for machining 316L include:
- Using sharp, robust cutting tools: Carbide tooling is often preferred for its hardness and wear resistance.
- Optimizing cutting speeds and feeds: Slower speeds and heavier feeds can help penetrate the work-hardened layer, reducing further hardening.
- Employing ample cutting fluid: This helps dissipate heat, lubricate the cutting zone, and aid in chip evacuation, preventing tool buildup and improving surface finish.
- Rigid setups: Minimizing vibration is crucial to maintain tool life and achieve high-quality surface finishes.
Precision Welding for 316L Stainless Steel
Welding is arguably the most critical stage in 316L stainless steel fabrication, directly impacting the final product's structural integrity and corrosion resistance. The low carbon content of 316L is a significant advantage, reducing the risk of sensitization—a phenomenon where chromium carbides precipitate at grain boundaries due to elevated temperatures, diminishing corrosion resistance. However, specific techniques and practices are vital to fully leverage this benefit.
Common Welding Methods and Their Application
While several welding processes can be employed for stainless steels, for 316L, Gas Tungsten Arc Welding (GTAW), commonly known as TIG welding, is frequently the method of choice, especially for applications demanding high-quality, clean welds. TIG welding, often performed with argon shielding gas, offers precise heat control and produces welds with excellent aesthetic quality and metallurgical integrity. This is particularly important for hygiene-sensitive industries where smooth, defect-free weld beads are essential for easy cleaning and to prevent microbial growth.
Maintaining Integrity: Controlling Heat Input
The primary concern during 316L welding is managing heat input. Excessive heat can still lead to undesirable microstructural changes, including grain growth or localized sensitization, despite the low carbon content. Best practices include:
- Lower Amperage and Faster Travel Speeds: This minimizes the heat-affected zone (HAZ) and reduces the overall heat input into the material.
- Interpass Temperature Control: Allowing the weldment to cool between passes is crucial. This prevents excessive heat buildup, which can lead to distortion and metallurgical degradation.
- Proper Filler Material Selection: Using an appropriate filler metal, often 316L or a similar low-carbon, molybdenum-containing alloy, ensures the weld metal's corrosion resistance matches or exceeds that of the base material.
- Shielding Gas Purity: Utilizing high-purity argon for TIG welding is essential to prevent atmospheric contamination (like oxygen and nitrogen) from entering the weld pool, which can lead to porosity and reduce corrosion resistance.
Best Practices for Weld Precision and Finish
Achieving high-quality, durable, and clean welds in 316L fabrication demands meticulous attention to detail. Professional TIG/Argon welding, combined with specific weld finishing techniques, is a demonstrated best practice. For instance, achieving a 120-grit weld finishing ensures a smooth surface that aligns with hygiene requirements and improves the aesthetic appeal of the fabricated component. Post-weld cleaning, such as wire brushing with stainless steel brushes (never carbon steel), and pickling or passivation, are often necessary to restore the passive layer and enhance the weld's corrosion resistance.
Addressing Fabrication Challenges for 316L
Fabricating 316L stainless steel presents distinct challenges that require specialized knowledge and approaches. Overcoming these ensures the final product meets the stringent performance and quality expectations.
Ensuring Hygiene and Contamination Prevention
In industries like food processing and pharmaceuticals, the prevention of contamination is non-negotiable. 316L's role in direct product contact equipment means its surfaces must be impeccably clean and smooth. During fabrication, any contact with carbon steel tools, dust, or particles can embed iron into the stainless steel surface. This embedded iron can rust and become a source of contamination or a nucleation site for corrosion, undermining the very reason 316L was chosen. Best practices include:
- Dedicated Fabrication Areas: Creating separate zones for 316L fabrication, isolated from carbon steel work, can significantly reduce cross-contamination risk.
- Exclusive Tooling: All tools—cutters, dies, brushes, clamps—should be made of stainless steel or be specifically designated for 316L work to prevent iron transfer. Even the work surface itself should be stainless steel or covered appropriately.
- Cleanliness Protocols: Regular cleaning of equipment and work areas is essential.
Achieving High-Quality Surface Finishes
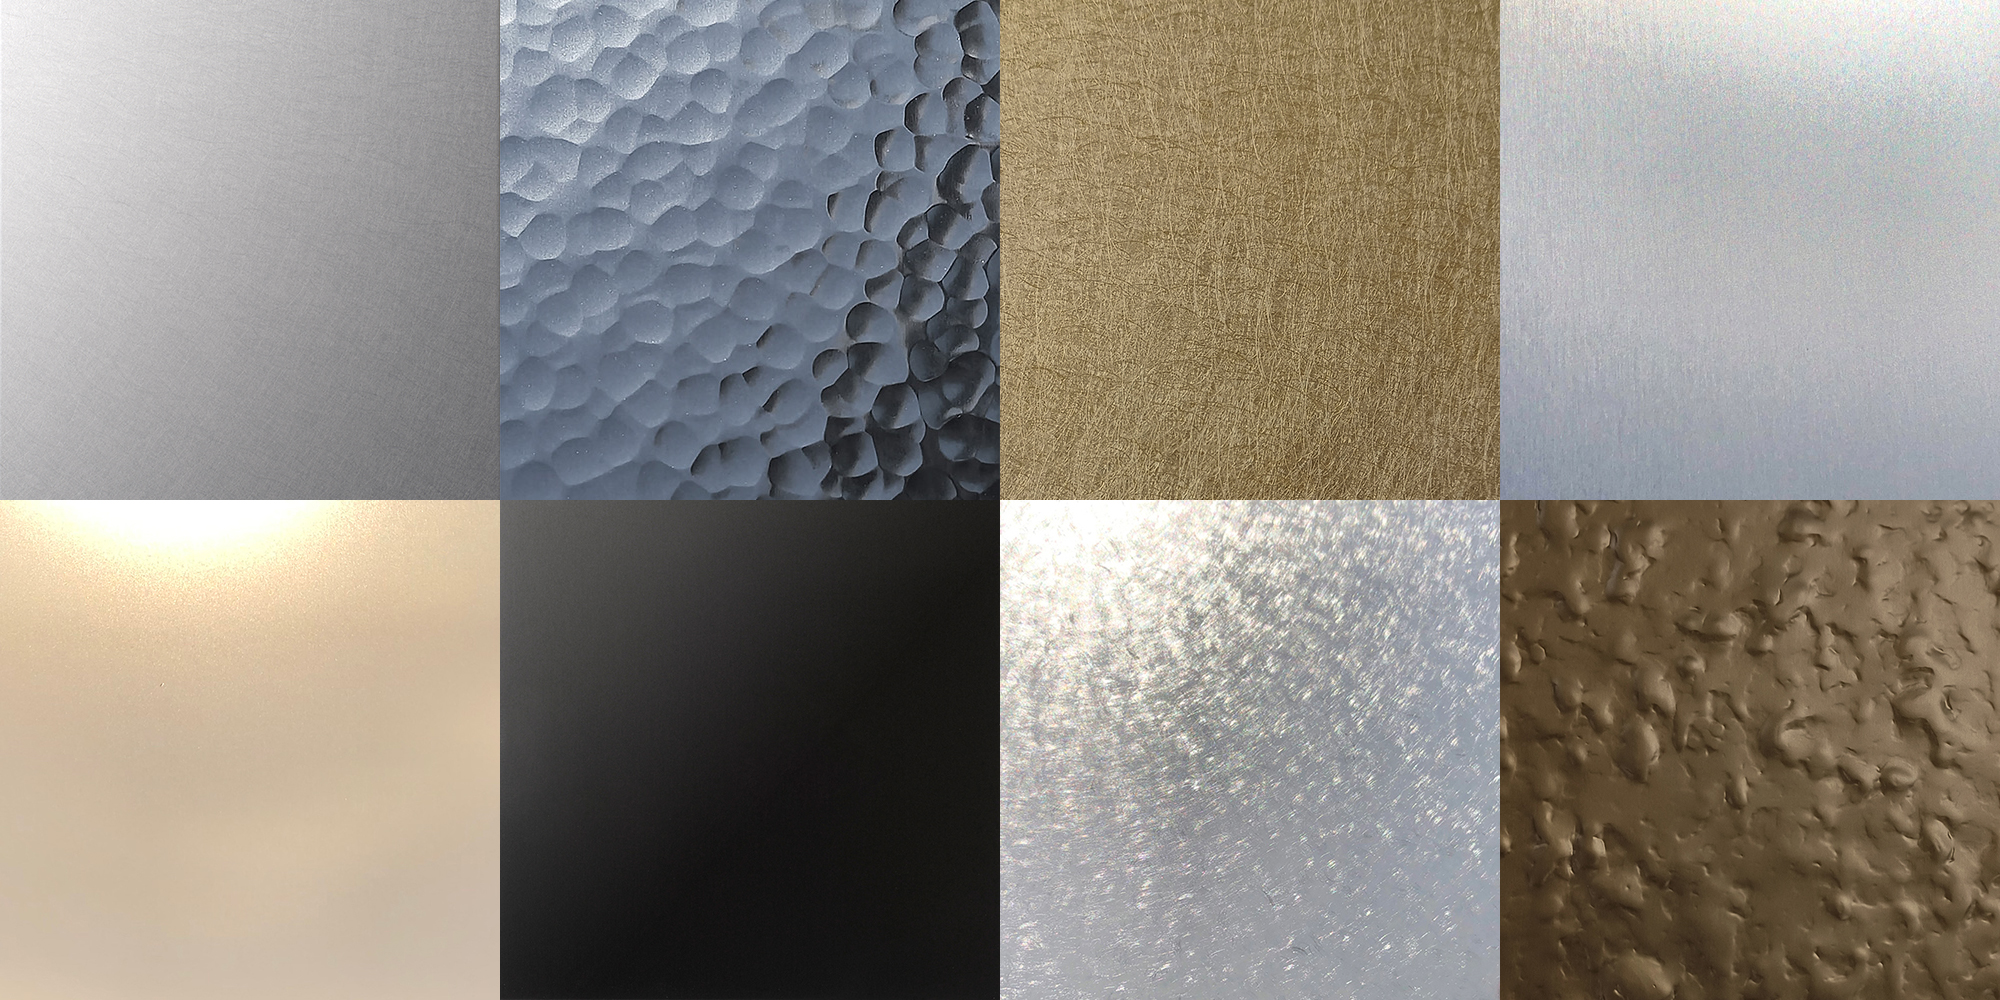
The surface finish of 316L components is critical not only for aesthetics but also for functionality, especially in hygiene-sensitive applications. A smooth, even surface is easier to clean, less prone to harboring bacteria, and more resistant to corrosion. Fabrication methods can significantly impact the final finish. Welding, grinding, and polishing must be executed precisely to eliminate crevices, imperfections, and surface roughness. The goal is often to achieve a uniform finish, specified by grit sizes (e.g., 120-grit, 240-grit) or Ra (roughness average) values, depending on the application. This process requires skilled operators and specialized equipment to avoid localized overheating or material removal that could introduce new imperfections.
Minimizing Distortion and Material Degradation
Stainless steels, including 316L, are prone to distortion during thermal processes like welding due to their lower thermal conductivity and higher thermal expansion coefficient compared to carbon steels. This can lead to warping or misalignment, necessitating costly corrective actions. To minimize distortion:
- Careful Design: Incorporating design features that distribute stress and rigidity can help.
- Controlled Welding Sequences: Employing skip welding or balanced welding techniques can reduce localized heat buildup.
- Clamping and Fixturing: Robust clamping and fixturing hold the material in place during welding, limiting movement.
- Material Degradation: Overheating can cause discoloration ("heat tint" or "sugaring") in the weld zone, which is a thin layer of oxidized chromium. While visually undesirable, this layer also indicates a depletion of chromium at the surface, reducing corrosion resistance. It must be removed, typically through mechanical abrasion followed by chemical cleaning.
Best Practices for Optimized 316L Stainless Steel Fabrication
To truly master 316L stainless steel fabrication, adopting a holistic approach that integrates best practices across all stages is vital.
Comprehensive Quality Control
Implementing rigorous quality control checks throughout the fabrication process is non-negotiable. This includes:
- Pre-Fabrication Inspection: Verifying material certifications and inspecting incoming raw materials for surface defects or contamination.
- In-Process Checks: Regular dimensional checks after cutting, forming, and machining. Visual inspection of weld beads for uniformity, penetration, and freedom from defects.
- Post-Fabrication Testing: For critical applications, this may involve non-destructive testing (NDT) methods like liquid penetrant inspection (LPI) for surface cracks, or radiographic testing for internal weld defects. Additionally, surface roughness measurements and passivation testing (e.g., copper sulfate test) ensure the final surface quality and corrosion resistance meet specifications.
Advanced Finishing and Post-Fabrication Treatments
Beyond mechanical polishing, several chemical and electrochemical treatments are crucial for enhancing 316L's performance:
- Pickling: This involves using acid solutions to remove heat tint, scale, and surface contaminants left after welding or heat treatment. It effectively restores the chromium-rich surface layer.
- Passivation: This is a chemical treatment, typically with nitric acid or citric acid, that removes free iron from the surface and promotes the spontaneous formation of a continuous, inert, chromium-rich passive layer. This layer is what gives stainless steel its corrosion resistance. Passivation is essential, especially after any mechanical or thermal processing that might disrupt the native passive layer.
- Electropolishing: An electrochemical process that selectively removes surface material, creating an extremely smooth, bright, and microscopically clean surface. Electropolishing significantly improves corrosion resistance, enhances cleanability, and often provides a highly aesthetic finish. It is particularly valued for medical and pharmaceutical components where ultra-smooth surfaces are critical.
These treatments are not merely cosmetic; they are fundamental to restoring and maximizing the intrinsic corrosion resistance of the 316L material after the fabrication processes. Understanding how various alloy steel treatments differ can further highlight the specialized nature of 316L finishing.
Conclusion: Continuous Improvement in 316L Fabrication
Mastering 316L stainless steel fabrication is an ongoing journey that combines scientific understanding with practical expertise. The unique properties of 316L demand a methodical approach, from material selection and handling to precision welding and advanced post-fabrication treatments. Adhering to best practices in contamination control, heat management, and surface finishing is not merely about achieving a product; it's about preserving and enhancing the inherent qualities that make 316L indispensable in demanding applications.
As industries evolve, so too will the techniques and demands placed on fabricators. Staying abreast of innovations in welding technology, machining processes, and surface treatment methods will be crucial for fabricators aiming to push the boundaries of what is possible with this remarkable material. The next steps for any fabricator looking to excel in this field involve investing in specialized training, acquiring advanced equipment, and fostering a culture of meticulous quality control to meet the exacting standards required for 316L components.
