Optimizing Metal Finishing Pretreatment: A Technical Guide to Enhanced Performance and Compliance (Updated 2026-11-18)
For manufacturers and engineers in metal fabrication, the longevity and performance of a finished product often hinge on a stage that remains largely unseen: surface preparation. It is not uncommon for challenges like peeling paint, premature corrosion, or inconsistent finishes to arise, leading to costly rework or reputational damage. While the final coating or plating process typically garners attention, the critical foundation for success—metal finishing pre-treatment—is where the real work of ensuring durability and quality begins. This comprehensive technical guide aims to demystify the complex world of pre-treatment, explaining its underlying principles, diverse processes, and the optimization strategies essential for superior outcomes in 2026.
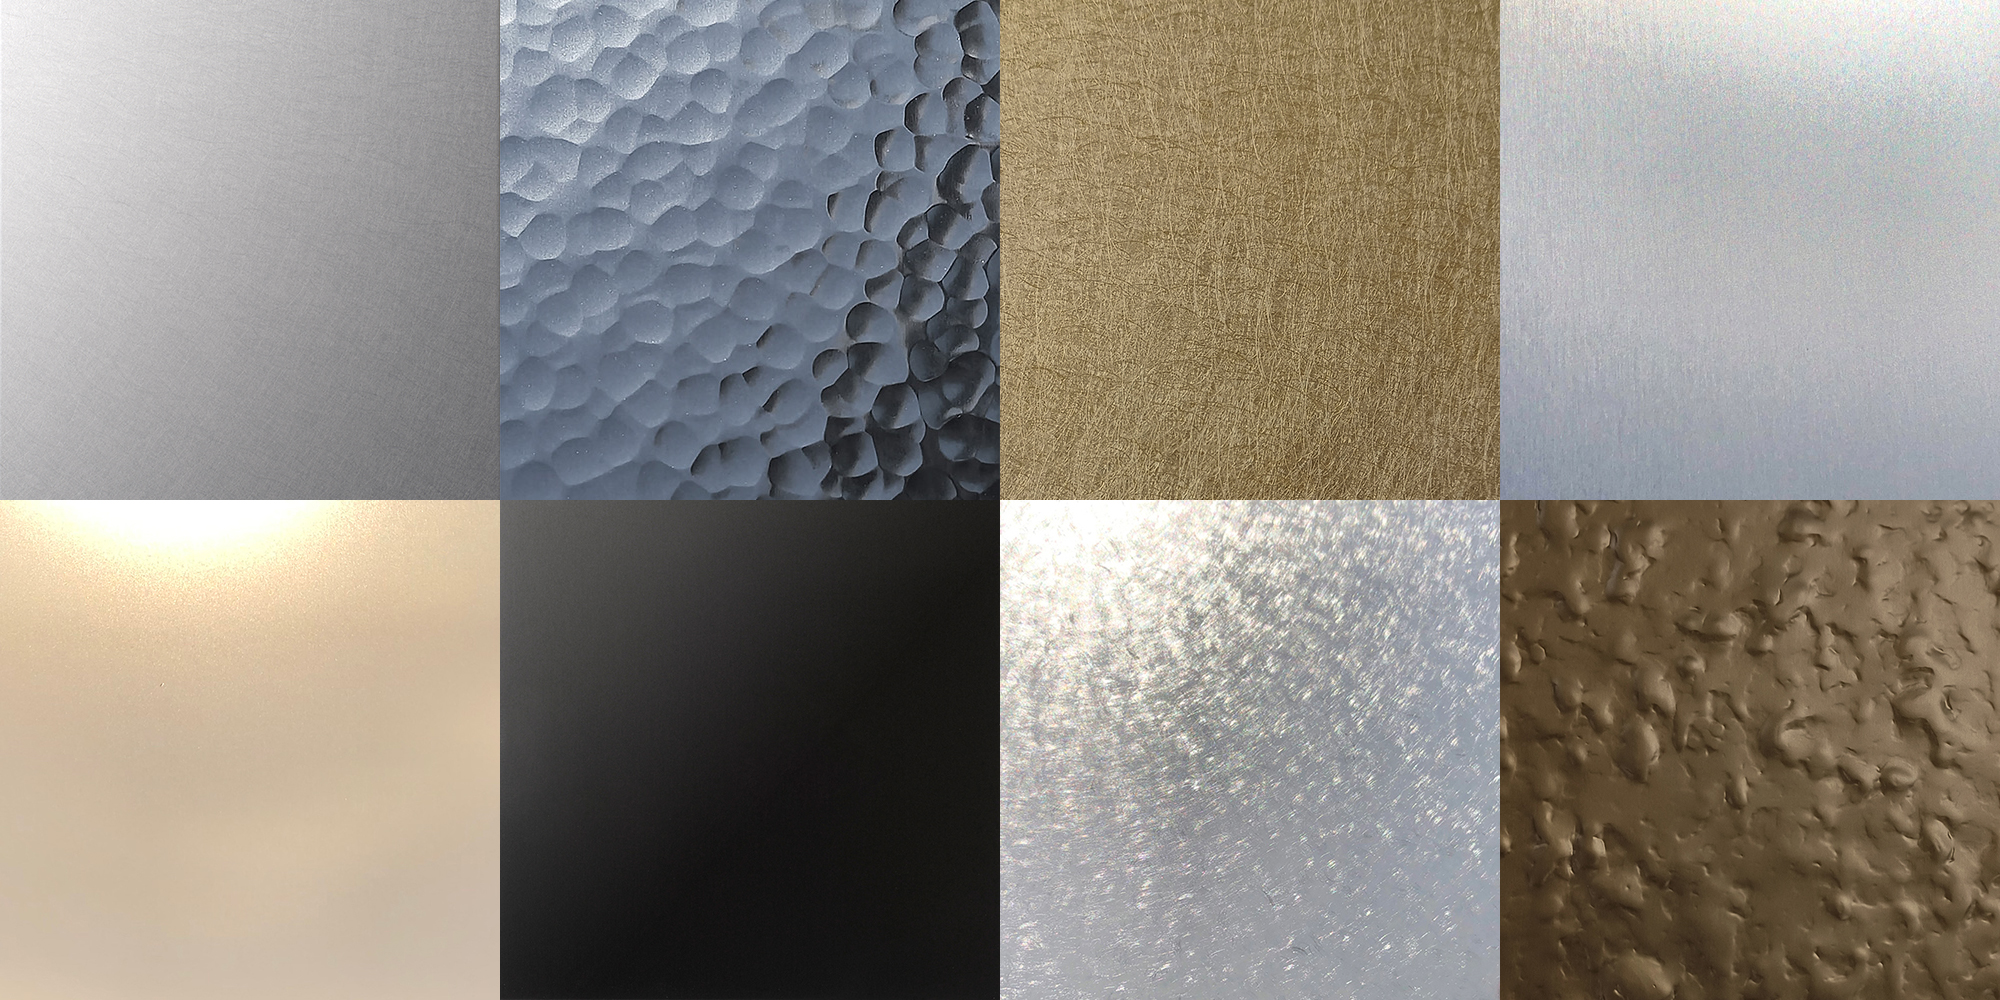
Pre-treatment is far more than a simple cleaning step; it is a meticulously engineered sequence designed to transform a metal surface into an ideal canvas for subsequent finishing operations. Its importance cannot be overstated, influencing everything from coating adhesion and corrosion resistance to the overall lifespan of the finished part.
The Dual Role of Pretreatment: Technical Surface Preparation vs. Environmental Compliance
Effective metal finishing pre-treatment serves two fundamentally distinct yet equally critical functions. Understanding this duality is crucial for comprehensive optimization.
Defining Technical Pretreatment for Product Quality
Technical pre-treatment focuses on preparing the metal surface itself. Its primary objective is to create a pristine, chemically reactive, and structurally suitable substrate for the application of subsequent coatings, platings, or other finishes. This involves the meticulous removal of contaminants such as oils, greases, dust, rust, and other oxides, which, if left unchecked, would compromise the adhesion and integrity of the final finish. Beyond cleaning, technical pre-treatment often includes chemical conversion processes that modify the metal's surface layer, enhancing properties like corrosion resistance and paint adhesion. Without proper technical pre-treatment, even the most advanced coatings will fail to achieve their intended performance, leading to defects, reduced product lifespan, and ultimately, customer dissatisfaction.
Environmental Pretreatment: Safeguarding Operations and the Environment
Parallel to technical preparation, environmental pre-treatment addresses the responsible management of industrial wastewater generated during metal finishing operations. This aspect is compliance-driven, ensuring that waste streams containing heavy metals, chemicals, and other pollutants are treated to meet strict regulatory standards before discharge. In the United States, regulations established by the U.S. Environmental Protection Agency (EPA), particularly the National Pretreatment Program under the Clean Water Act (40 CFR Parts 403 and 433), mandate specific limits for pollutants discharged to Publicly Owned Treatment Works (POTWs). Facilities must invest in sophisticated wastewater treatment systems to remove or neutralize harmful substances, protecting public health and the environment from contamination.
The Critical Consequences of Pretreatment Failure
Failure in either domain carries significant consequences. Inadequate technical pre-treatment results in commercial and reputational risks. Products may experience poor coating adhesion, blistering, or premature corrosion, necessitating costly rework, warranty claims, and loss of customer trust. Conversely, failures in environmental pre-treatment lead to severe legal and operational repercussions. Facilities face permit violations, substantial fines, and potential operational suspension or termination, highlighting the indispensable nature of compliance.
Essential Technical Pretreatment Processes for Optimal Metal Finishing
Achieving an optimal surface for metal finishing involves a sequence of carefully selected and controlled processes.
Comprehensive Cleaning and Degreasing Techniques
The first critical step in any metal finishing pre-treatment sequence is thorough cleaning. The presence of oils, greases, machining fluids, polishing compounds, and other organic or inorganic soils will invariably compromise coating adhesion. Common cleaning methods include:
- Alkaline Cleaning: This involves immersing parts in hot alkaline solutions (pH 9-14) containing surfactants, emulsifiers, and detergents. The high pH saponifies fats and oils, while surfactants lift and disperse other contaminants. Agitation, either mechanical or ultrasonic, often enhances efficiency.
- Acid Cleaning/Pickling: Used to remove rust, scale, and other inorganic oxides from the metal surface. Diluted acids like hydrochloric, sulfuric, or phosphoric acid dissolve these layers. Inhibitors are often added to minimize acid attack on the base metal.
- Solvent Cleaning: While increasingly regulated due to environmental concerns, solvent cleaning (e.g., with specific hydrocarbon or halogenated solvents) can be effective for rapid degreasing, particularly for localized cleaning or specific contaminant types.
- Mechanical Cleaning: Abrasive blasting (sandblasting, grit blasting), tumbling, or wire brushing mechanically removes heavy scale, rust, or existing coatings, providing a clean, roughened surface for better adhesion.
The Science of Conversion Coatings
Once a surface is clean, conversion coatings chemically alter the outermost layer of the metal substrate to create a more receptive surface. These coatings are typically thin, inorganic films that improve corrosion resistance and provide excellent adhesion for paints and other organic coatings.
- Phosphating: A widely used method, especially for steel and zinc, where the metal reacts with a phosphoric acid solution to form an insoluble crystalline phosphate layer. Iron phosphate, zinc phosphate, and manganese phosphate are common types, each offering different characteristics. Zinc phosphate, in particular, is known for its excellent corrosion resistance and robust base for powder coating.
- Chromating: Historically, chromate conversion coatings (containing hexavalent chromium) offered exceptional corrosion resistance for aluminum, magnesium, and zinc. However, due to health and environmental concerns regarding hexavalent chromium, trivalent chromium alternatives are now widely adopted. These newer technologies provide comparable performance with significantly reduced environmental impact.
- Anodizing: Primarily used for aluminum and its alloys, anodizing is an electrolytic passivation process that increases the thickness of the natural oxide layer on the metal surface. This dense, porous oxide layer can be dyed, sealed, and provides excellent corrosion and wear resistance.
Full Immersion Systems Versus Spray Systems
The method of applying pre-treatment chemicals significantly impacts outcome quality.
- Spray Systems: Parts are conveyed through a series of enclosed tunnels where chemicals are sprayed onto their surfaces. This method can be energy-efficient for large volumes of simple geometries and offers precise control over chemical application. However, spray systems can struggle to reach recessed areas, complex geometries, or welded assemblies, potentially leading to incomplete coverage and compromised adhesion.
- Full Immersion Systems: In these systems, parts are fully submerged in tanks containing the pre-treatment chemicals. This ensures complete wetting and penetration into all crevices, blind holes, and complex profiles, providing superior surface coverage and robust adhesion. For applications demanding the highest quality, longevity, and warranty validity, full immersion is often considered the superior choice. An example is a 7-stage full immersion system used for complex parts, guaranteeing thorough cleaning and conversion coating.
Navigating Metal Finishing Pre-treatment Regulations and Compliance
The regulatory landscape plays an equally vital role in shaping metal finishing pre-treatment operations.
U.S. EPA Metal Finishing Effluent Guidelines (40 CFR Part 433)
The U.S. EPA promulgated the Metal Finishing Effluent Guidelines in 1983, a set of regulations under 40 CFR Part 433, to control the discharge of pollutants from metal finishing facilities. These guidelines establish technology-based effluent limitations for various operations, including electroplating, electroless plating, anodizing, coating, chemical etching, and milling. Facilities performing one or more of these core operations are typically subject to these guidelines. Compliance requires careful monitoring and treatment of wastewater to reduce levels of heavy metals and other toxic substances before discharge.
The National Pretreatment Program (40 CFR Part 403)
Beyond the specific Metal Finishing Effluent Guidelines, the National Pretreatment Program (40 CFR Part 403) provides the framework for controlling industrial discharges into POTWs. This program requires industrial users to pre-treat their wastewater to remove pollutants that could interfere with the POTW's operation, pass through the POTW untreated into receiving waters, or contaminate sludge. Industrial facilities are often required to obtain permits and implement wastewater treatment systems tailored to their specific discharge characteristics, ensuring their pre-treatment operations meet local and federal standards. For many facilities, such as those providing a Cnc Machining Service, this means careful management of all process water.
Addressing Emerging Contaminants: PFAS and Hexavalent Chromium
Regulatory scrutiny of metal finishing waste streams is continually evolving. A significant current focus of the EPA involves addressing per- and polyfluoroalkyl substances (PFAS) discharges from chrome finishing facilities. PFAS compounds have historically been used in these facilities to control hexavalent chromium emissions, which are highly toxic. As understanding of PFAS's environmental persistence and health effects grows, regulations are emerging to limit their release. This necessitates that facilities employing such chemistries explore alternative, PFAS-free solutions to ensure future compliance and reduce environmental impact. For specific materials like Alloy Steel, the appropriate pre-treatment must balance performance with these evolving environmental considerations.
Advanced & Sustainable Pretreatment Solutions for Modern Manufacturing
The industrial landscape is moving towards more environmentally conscious and economically efficient practices. This shift is profoundly impacting metal finishing pre-treatment.
Reassessing Traditional Pretreatment Methods
Traditional multi-stage pre-treatment methods, while effective, often present significant challenges. Conventional phosphating processes, for instance, typically involve multiple heated chemical stages, extensive rinsing, and the generation of considerable volumes of hazardous sludge and complex waste streams. These methods are resource-intensive, requiring substantial energy for heating and large quantities of water for rinsing. The use of heavy metals and other harmful substances also contributes to a higher environmental footprint and increased costs associated with waste disposal.
Innovative, Eco-Friendly Technologies
The demand for sustainability has driven the development of advanced pre-treatment solutions that address these drawbacks. Emerging technologies offer compelling alternatives:
- One-Step Chemistries: These formulations combine cleaning and conversion coating into a single bath, significantly reducing the number of process stages, equipment footprint, and overall cycle time.
- Non-Toxic Formulations: Modern chemistries often eliminate or drastically reduce the use of heavy metals (like chromium) and other hazardous substances, making operations safer for workers and minimizing environmental risk.
- Rinse-Free Processes: Some innovative solutions are designed to be "rinse-free," eliminating the need for copious amounts of rinse water, thereby conserving water resources and drastically reducing wastewater generation.
- Ambient Temperature Operation: Moving away from heated baths to ambient temperature processes dramatically cuts energy consumption, leading to lower operational costs and a reduced carbon footprint.
These advancements demonstrate a clear path toward more sustainable manufacturing. By adopting such innovations, facilities can not only meet stringent environmental regulations but also improve operational efficiency and competitiveness in the long term. Further information on such sustainable practices can be found at www.bingzhen-sh.com.
Frequently Asked Questions
What chemicals are used for pretreatment in powder coating?
Traditional pre-treatment methods for powder coating often involve multiple heated chemical stages, including alkaline cleaners, various types of rinses, and conversion coatings like phosphating (e.g., zinc phosphate or iron phosphate). Emerging solutions, however, are shifting towards non-toxic, one-step chemistries that combine cleaning and conversion, reducing the environmental impact and simplifying the process.
What are two surface treatments for metal?
Two common surface treatments for metal that often rely on robust pre-treatment are electroplating and anodizing. Electroplating involves depositing a thin layer of one metal onto another for corrosion resistance or aesthetic purposes. Anodizing, predominantly used for aluminum, creates a protective oxide layer on the surface through an electrochemical process.
